Commercial & Engineering Sourcing Guide

Custom Humanoid Actuator Cost Reduction

Compare batch costs and tooling NRE, then prepare a same-scope RFQ.

Batch cost + NRE

Fictional USD inputs. Edit quantity to compare batch costs.

Illustrative cost model inputs and results

1–50,000 whole units. Batch size does not select a production stage.

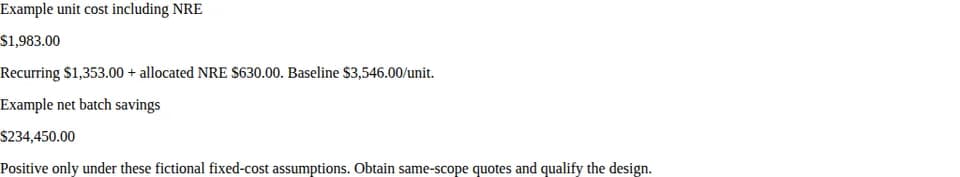
Example unit cost including NRE

$1,983.00

Recurring $1,353.00 + allocated NRE $630.00. Baseline $3,546.00/unit.

Example net batch savings

$234,450.00

Positive only under these fictional fixed-cost assumptions. Obtain same-scope quotes and qualify the design.

Architecture assumptions (required selections, defaults prefilled)

These options change fictional coefficients. No motor sizing, performance equivalence, price validation or safety qualification is performed.

Your supplier quote (optional, separate from example)

Enter both amounts or leave both blank. USD, up to 2 decimal places. Enter NRE 0 only when confirmed. Limits: unit $10,000,000; NRE $1,000,000,000.

No complete valid quote entered. Example costs are not used to fill missing quote values.

Example recurring-cost reduction: 61.84% before NRE. Package NRE: $94,500.00. Package payback: 44 units at fixed process assumptions. This is not a stator-only threshold.

Model assumptions and formulas (fictional USD inputs)

Recurring cost = sum of rounded baseline × coefficient. Effective unit cost = recurring + NRE/Q. Net batch savings = Q × (baseline − recurring) − NRE. Payback = ceil(NRE / positive recurring savings). Baseline has zero incremental NRE. Displayed money is rounded to cents.

Selected assumptions, reviewed 2026-11-02. No market calibration.
SubsystemBaseline USDCoefficientRecurring USDNRE USD
Transmission1,232.500.45555.0012,000.00
Motor797.500.38303.0022,000.00
Position sensing240.000.2458.007,500.00
Housing and bearings696.000.32223.0026,000.00
Driver and harness320.000.36115.0015,000.00
Assembly and EOL260.000.3899.0012,000.00

Example recurring cost by subsystem

Transmission$555.00 (41%, rounded)

Validate ratio, fatigue, shock loads and efficiency using a supplier-sized assembly.

Motor$303.00 (22%, rounded)

Confirm tooling ownership, winding feasibility and hot demagnetization margin.

Position sensing$58.00 (4%, rounded)

Measure installed accuracy, temperature drift and fault detection; resolution alone is insufficient.

Housing and bearings$223.00 (16%, rounded)

Retain qualified hardened steel raceways; validate preload, fits and thermal expansion.

Driver and harness$115.00 (8%, rounded)

Validate thermal coupling, EMI, regeneration and required safety functions.

Assembly and EOL$99.00 (7%, rounded)

Time a validated production screen; qualify thermal equilibrium and life separately.

Interpretation and limits

  • All model prices, multipliers and NRE are fictional assumptions. No supplier data or performance equivalence is established. Use itemized quotes before committing spend.
  • Process maturity is independent of this batch quantity. Changing quantity only changes NRE allocation and totals; it does not create a supplier volume discount.
  • The baseline assumes zero incremental NRE. Package payback excludes redesign, validation, scrap, freight, tax, financing and service costs; it is not a stator-only tooling threshold.

Next steps before spending

  • Request same-scope itemized quotes for recurring unit cost, one-time tooling, assembly, testing and expected yield.
  • Freeze torque-speed duty, cooling, life, output accuracy and fault-response requirements before comparing architecture costs.
  • Use separate tooling payback for each subsystem: incremental NRE / verified per-unit savings. Keep steel bearing rings unless a bearing specialist qualifies a replacement.
Request a DFM and quotation review

Report Created:

Engineering Audit:

Maintained by Custom Humanoid Actuator

Technical Chapter

1. Decide on total batch cost before unit BOM

Compare the complete cost scopeRecurring cost: Six complete buckets: Same acceptance scope; Incremental NRE: Tooling + validation: Allocate to real volume; Batch decision: Compare total costs: Qualify before release. Decision flow, not a measured cost distribution. Normalize scope before comparing savings.Recurring costSix complete bucketsSame acceptance scopeIncremental NRETooling + validationAllocate to real volumeBatch decisionCompare total costsQualify before release
Compare the complete cost scope. Decision flow, not a measured cost distribution. Normalize scope before comparing savings. Scroll horizontally on small screens.

Core Engineering Conclusion

Reduce recurring cost only after accounting for one-time tooling and qualification. A cheaper proposed BOM can still make a small batch more expensive.

Evidence, Method & Assumptions

Illustrative arithmetic: baseline $1,000/unit, proposed $700/unit, incremental NRE $30,000. At 50 units the proposal totals $65,000 versus $50,000 baseline; at 200 units it totals $170,000 versus $200,000. Payback is 100 units. These are invented examples, not market benchmarks.

Decide on total batch cost before unit BOM — decision comparison (reviewed 2026-11-02)
DecisionKnown calculationEvidence still needed
Recurring savingsBaseline unit cost − proposed unit costComparable torque-speed duty and acceptance scope
Batch savingsQ × recurring savings − incremental NRECommitted quantity, tooling ownership and change costs
Release decisionCost plus qualification readinessMeasured thermal, accuracy, fatigue and fault response
Engineering Boundary & Caveat:No verified public dataset establishes a universal humanoid actuator cost share or sub-$500 target. Actual supplier prices and achieved savings are unknown.
Recommended Sourcing Action:Set a same-scope baseline, obtain quotes and reject savings that disappear after NRE, yield, logistics and validation.
Prepare a same-scope cost reduction RFQ
Technical Chapter

2. Normalize six cost buckets

Compare the complete cost scopeRecurring cost: Six complete buckets: Same acceptance scope; Incremental NRE: Tooling + validation: Allocate to real volume; Batch decision: Compare total costs: Qualify before release. Decision flow, not a measured cost distribution. Normalize scope before comparing savings.Recurring costSix complete bucketsSame acceptance scopeIncremental NRETooling + validationAllocate to real volumeBatch decisionCompare total costsQualify before release
Compare the complete cost scope. Decision flow, not a measured cost distribution. Normalize scope before comparing savings. Scroll horizontally on small screens.

Core Engineering Conclusion

Require identical scope across offers. A reducer-only price cannot be compared with a tested actuator module.

Evidence, Method & Assumptions

Procurement method: reconcile transmission, motor, feedback, structure/bearings, electronics/harness, and assembly/test. The tool exposes a fictional baseline, multiplier and NRE for each bucket; standards are not price sources.

Normalize six cost buckets — decision comparison (reviewed 2026-11-02)
BucketMust includeCommon hidden addition
Transmission and motorReducer/screw, stator, rotor and retentionMatching, balancing and tooling
Feedback and electronicsSensors, calibration, inverter and harnessFirmware license, calibration fixture and EMC work
Housing and assemblyQualified bearings, seals, assembly and EOLPreload adjustment, rework and life validation
Engineering Boundary & Caveat:Recurring BOM estimates exclude margin, freight, tariffs, scrap and service unless the quote explicitly includes them.
Recommended Sourcing Action:Ask suppliers to mark inclusions and exclusions against the same drawing revision and acceptance plan.
Technical Chapter

3. Select transmission by the load envelope

Transmission substitution needs system resizingOutput requirement: Torque + speed + shock: Lost motion + life; System sizing: Ratio + motor + cooling: Bearings + controls; Release gate: Loaded qualification: Then compare cost. Architecture labels cannot establish equal torque, thermal performance, accuracy or service life.Output requirementTorque + speed + shockLost motion + lifeSystem sizingRatio + motor + coolingBearings + controlsRelease gateLoaded qualificationThen compare cost
Transmission substitution needs system resizing. Architecture labels cannot establish equal torque, thermal performance, accuracy or service life. Scroll horizontally on small screens.

Core Engineering Conclusion

Compare transmission architectures only after sizing motor, reducer, bearings and cooling to the same output requirement.

Evidence, Method & Assumptions

Engineering inference: changing ratio changes required motor torque and speed. Gear stiffness, hysteresis and efficiency must be obtained at the intended load rather than inferred from an architecture label.

Select transmission by the load envelope — decision comparison (reviewed 2026-11-02)
ArchitectureDecision advantage to investigateValidation gate
Strain waveCompact high reductionFlexspline fatigue and load-dependent hysteresis
Low-ratio planetary / QDDBackdrivability with a different motor envelopeMotor current, thermal limits and backlash
CycloidalAlternative stiffness and load pathRipple, bearing loads, mass and supplier life calculation
Engineering Boundary & Caveat:The calculator changes cost coefficients but does not resize a motor or predict fatigue, backlash, shock survival or efficiency. Its alternatives are not equal-performance designs.
Recommended Sourcing Action:Send the load spectrum, permissible lost motion, ratio, speed, space and shock requirements for a part-specific selection.
Technical Chapter

4. Separate lamination tooling from package payback

Stator-specific tooling paybackIncremental die NRE: $20,000 assumption: Confirm maintenance; Per-stack saving: $160 assumption: Same stack geometry; Payback: 125 stacks: Before extra costs. Fictional example: $20,000 / ($180 − $20) = 125 stacks. This differs from whole-package payback.Incremental die NRE$20,000 assumptionConfirm maintenancePer-stack saving$160 assumptionSame stack geometryPayback125 stacksBefore extra costs
Stator-specific tooling payback. Fictional example: $20,000 / ($180 − $20) = 125 stacks. This differs from whole-package payback. Scroll horizontally on small screens.

Core Engineering Conclusion

Do not buy a stamping die until its own incremental tooling and verified stack savings justify it.

Evidence, Method & Assumptions

Illustrative stator example: $20,000 incremental die cost / ($180 laser stack − $20 stamped stack) = 125 stacks. These invented inputs explain the method; the tool’s package payback includes six subsystems and is a different number.

Separate lamination tooling from package payback — decision comparison (reviewed 2026-11-02)
RouteCost mechanismRelease evidence
Laser-cut stackAvoid dedicated hard tooling during revisionsBurrs, interlaminar insulation and stack loss
Stamped stackExchange tooling spend for recurring savingsDie life, stack dimensional capability and steel utilization
Magnet/process substitutionPotential material or process changeTemperature-dependent demagnetization curve and assembly test
Engineering Boundary & Caveat:Die maintenance, material utilization, burr control, core losses, winding changes and engineering revisions can shift payback. Magnet grade labels alone do not establish hot demagnetization margin.
Recommended Sourcing Action:Obtain laser and stamping quotes for the same stack; require hot operating-point data for any low-heavy-rare-earth magnet substitution.
Technical Chapter

5. Buy installed accuracy and diagnostic coverage

Measure installed feedback performanceSensor + target: Alignment and runout: Optical / inductive / Hall; Calibration: Installed error map: Temperature and EMI; Task acceptance: Output error budget: Fault response testing. Resolution is not installed accuracy. Validate temperature, load, alignment and required diagnostics.Sensor + targetAlignment and runoutOptical / inductive / HallCalibrationInstalled error mapTemperature and EMITask acceptanceOutput error budgetFault response testing
Measure installed feedback performance. Resolution is not installed accuracy. Validate temperature, load, alignment and required diagnostics. Scroll horizontally on small screens.

Core Engineering Conclusion

Compare encoders by installed error and required output observation, rather than bit count or a universal price claim.

Evidence, Method & Assumptions

Engineering inference: disc/ring runout, eccentricity, magnetic environment, temperature and calibration affect installed error. Single-input sensing cannot directly observe output compliance or lost motion.

Buy installed accuracy and diagnostic coverage — decision comparison (reviewed 2026-11-02)
ArchitectureCost/packaging questionAcceptance evidence
Dual opticalPackaging, alignment and protection needsInstalled error over temperature and vibration
Dual inductive/magneticTargets, calibration and EMI needsResidual error map and fault injection
Single inputLower component count versus output observabilityTask-specific error budget and safety assessment
Engineering Boundary & Caveat:No calibration dataset is supplied here. Optical, inductive and magnetic options have no universal accuracy ranking, and dual sensors alone do not establish functional safety.
Recommended Sourcing Action:Specify output accuracy across load and temperature, calibration residuals, production cycle time and fault response before deleting feedback.
Technical Chapter

6. Consolidate housing features while retaining qualified raceways

Housing consolidation with qualified bearing ringsCast / CNC shell: Locate steel rings: Common datums; Steel raceways: Qualified material: Preload and retention; Loaded validation: Fits over temperature: Wear and fatigue life. Retain hardened steel rolling surfaces. A cast bearing seat is not a rolling raceway.Cast / CNC shellLocate steel ringsCommon datumsSteel racewaysQualified materialPreload and retentionLoaded validationFits over temperatureWear and fatigue life
Housing consolidation with qualified bearing rings. Retain hardened steel rolling surfaces. A cast bearing seat is not a rolling raceway. Scroll horizontally on small screens.

Core Engineering Conclusion

A cast aluminium or magnesium shell can locate a steel bearing ring. It must not be assumed to replace the hardened rolling surface.

Evidence, Method & Assumptions

Schaeffler’s material guidance requires adequate raceway hardness and hardened depth for load capacity. Our design inference is to retain qualified steel rings unless a bearing specialist validates another construction.

Consolidate housing features while retaining qualified raceways — decision comparison (reviewed 2026-11-02)
Housing routePotential saving mechanismConstraint / alternative
CNC billet + steel ringsLow tooling commitment during design changesOptimize setups and common datums
Cast shell + steel ringsNear-net geometry and fewer machining operationsValidate porosity, bore capability and bearing fits
Raceway integrated into qualified steel structurePotential part-count reductionSpecialist material, heat-treatment and life qualification required
Engineering Boundary & Caveat:Direct rolling on an unqualified soft casting risks wear, deformation and preload loss. Casting changes also alter porosity, stiffness, fits and thermal expansion.
Recommended Sourcing Action:Consolidate flanges and fasteners first; release bearing interfaces only after supplier review and loaded thermal cycling.
Technical Chapter

7. Verify thermal changes before downsizing

Thermal change requires a matched comparisonBaseline test: Same torque-speed duty: Same ambient + mount; Potting trial: Void and cure control: Measure winding hotspot; Cost decision: Include cure and scrap: Downsize only if proven. No measured torque uplift is claimed. Material conductivity does not equal assembly thermal resistance.Baseline testSame torque-speed dutySame ambient + mountPotting trialVoid and cure controlMeasure winding hotspotCost decisionInclude cure and scrapDownsize only if proven
Thermal change requires a matched comparison. No measured torque uplift is claimed. Material conductivity does not equal assembly thermal resistance. Scroll horizontally on small screens.

Core Engineering Conclusion

Potting may change the heat path, but a material conductivity value alone does not justify a smaller motor.

Evidence, Method & Assumptions

Engineering inference: interfaces, voids, winding geometry and cooling determine assembly thermal resistance. Compare measured winding rise at the same duty, ambient and mounting boundary.

Verify thermal changes before downsizing — decision comparison (reviewed 2026-11-02)
OptionCost item to compareEvidence needed
Varnish / unpotted assemblyAssembly and repair accessWinding hotspot and insulation margin
Filled epoxy / pottingMaterial, vacuum, cure and inspectionVoid control, thermal cycling and hotspot comparison
Improved housing heat pathInterface and cooling hardwareMounting repeatability and equilibrium test
Engineering Boundary & Caveat:No before/after thermal measurements are available here. Torque uplift, frame reduction and return on investment remain unknown; potting can increase scrap and impair repairability.
Recommended Sourcing Action:Run instrumented A/B thermal tests and include dispense, cure, inspection and rework costs in the proposal.
Technical Chapter

8. Compare external and integrated drive service costs

Ideal DC input at fixed 1.2 kW48 V DC bus: 25 A input: Cable loss ratio 1.00; 72 V DC bus: 16.67 A input: Cable loss ratio 0.444; 96 V DC bus: 12.5 A input: Cable loss ratio 0.25. DC input only: P/V. Same cable resistance gives I²R ratios 1, 0.444, 0.25. Motor phase current is a separate calculation; no efficiency, mass or safety level is inferred.48 V DC bus25 A inputCable loss ratio 1.0072 V DC bus16.67 A inputCable loss ratio 0.44496 V DC bus12.5 A inputCable loss ratio 0.25
Ideal DC input at fixed 1.2 kW. DC input only: P/V. Same cable resistance gives I²R ratios 1, 0.444, 0.25. Motor phase current is a separate calculation; no efficiency, mass or safety level is inferred. Scroll horizontally on small screens.

Core Engineering Conclusion

Inverter integration can remove cable interfaces while adding heat and service coupling. Evaluate both effects.

Evidence, Method & Assumptions

Engineering inference: a shorter phase connection changes packaging, while an integrated board shares the motor’s thermal and mechanical environment. Semiconductor technology alone says nothing about achieved efficiency or safety level.

Compare external and integrated drive service costs — decision comparison (reviewed 2026-11-02)
PackagingPotential cost benefitCounter-cost / gate
External inverterAccessible service and thermal separationPhase harness, connectors and routing
Integrated inverterFewer external phase interfacesThermal coupling, EMI and module replacement
GaN versus siliconApplication-dependent switching trade-offMeasured total losses, overshoot and voltage margin
Engineering Boundary & Caveat:No verified efficiency map, harness mass measurement or validated safety design is provided. GaN does not automatically provide silent operation or PL d.
Recommended Sourcing Action:Compare measured losses across the duty map, EMI, regeneration, replacement labor and the complete safety concept.
Technical Chapter

9. Quote lead time instead of assuming a regional advantage

Verify supplier delivery and costDated offer: Scope + Incoterm: Validity + exclusions; Capacity evidence: Sub-tier bottlenecks: First-article milestones; Resilience plan: Qualified alternates: Tool transfer rights. No regional market share, dispatch speed or price advantage is asserted.Dated offerScope + IncotermValidity + exclusionsCapacity evidenceSub-tier bottlenecksFirst-article milestonesResilience planQualified alternatesTool transfer rights
Verify supplier delivery and cost. No regional market share, dispatch speed or price advantage is asserted. Scroll horizontally on small screens.

Core Engineering Conclusion

Supplier location alone does not establish cost, quality or delivery performance.

Evidence, Method & Assumptions

Procurement method: compare dated offers on material availability, bottleneck capacity, sub-tier traceability, transit and acceptance terms. Public evidence is insufficient for the former regional price and lead-time comparisons.

Quote lead time instead of assuming a regional advantage — decision comparison (reviewed 2026-11-02)
FactorKnown from a complete offerUnknown until verified
Unit and logistics costCurrency, Incoterm, destination and validityTariff classification and delivered charges
Lead timeMaterial, tooling, first article and production milestonesSub-tier capacity and qualification delays
ContinuityNamed process owners and approved alternativesRecovery time after a quality escape
Engineering Boundary & Caveat:No verified factory dispatch, capacity or geographical market-share data is supplied. Geography cannot replace process qualification.
Recommended Sourcing Action:Ask each bidder for a capacity reservation, dated lead-time breakdown, alternate-source plan and delivered-cost scope.
Technical Chapter

10. Separate EOL screening from design qualification

Production screening and qualification have different jobsQualification: Thermal equilibrium: Fatigue + environment; Production screen: Assembly + calibration: Selected loaded points; Periodic audit: Check screen correlation: Contain process drift. A short production screen does not prove continuous thermal capability or fatigue life.QualificationThermal equilibriumFatigue + environmentProduction screenAssembly + calibrationSelected loaded pointsPeriodic auditCheck screen correlationContain process drift
Production screening and qualification have different jobs. A short production screen does not prove continuous thermal capability or fatigue life. Scroll horizontally on small screens.

Core Engineering Conclusion

Automate a production screen without claiming that minutes of testing prove continuous thermal capability or service life.

Evidence, Method & Assumptions

Engineering inference: production screens can check electrical continuity, calibration and selected loaded points. Thermal equilibrium, fatigue and abuse validation require a separate qualification plan.

Separate EOL screening from design qualification — decision comparison (reviewed 2026-11-02)
Test layerPurposeCost boundary
Design qualificationThermal, fatigue and environmental capabilityEngineering samples and long-duration benches
Production EOLAssembly errors, calibration and selected performanceFixture time, maintenance and false rejects
Periodic auditDetect process drift and escapesSampling basis and containment response
Engineering Boundary & Caveat:A fixed 3.5-minute cycle cannot universally validate continuous torque. EOL time and first-pass yield are unknown until measured on the actual line.
Recommended Sourcing Action:Correlate the short screen against qualified reference units; retain periodic audit tests and serialize results.
Technical Chapter

11. Use explicit volume and NRE assumptions

Fixed NRE allocation — illustrative arithmetic50 units: $600 NRE / unit: $1,300 effective / unit; 100 units: $300 NRE / unit: $1,000 effective / unit; 200 units: $150 NRE / unit: $850 effective / unit. Invented $30,000 NRE and $700 recurring cost: quantity changes allocation, not recurring price.50 units$600 NRE / unit$1,300 effective / unit100 units$300 NRE / unit$1,000 effective / unit200 units$150 NRE / unit$850 effective / unit
Fixed NRE allocation — illustrative arithmetic. Invented $30,000 NRE and $700 recurring cost: quantity changes allocation, not recurring price. Scroll horizontally on small screens.

Core Engineering Conclusion

Increasing quantity spreads fixed NRE over more units; it does not by itself earn a lower recurring price.

Evidence, Method & Assumptions

Tool method: proposed recurring cost = sum of rounded baseline × selected coefficient. NRE = sum of subsystem NRE. Effective unit cost = recurring + NRE/Q. Net batch savings = Q × (baseline − recurring) − NRE.

Use explicit volume and NRE assumptions — decision comparison (reviewed 2026-11-02)
MetricFormulaInterpretation
Package paybackceil(NRE / positive recurring saving)No payback if recurring saving ≤ 0; not a subsystem threshold
Effective unit costProposed recurring + NRE/QMakes small-batch tooling penalties visible
User quote subtotalQ × entered price + entered NRESeparate arithmetic, excluding unquoted fees; enter both amounts
Engineering Boundary & Caveat:All example coefficients are invented and disclosed in the tool. Stage choices represent process assumptions, independent of batch quantity. No fitted market scaling curve is used.
Recommended Sourcing Action:Replace the discussion example with dated same-scope offers; calculate each batch and downside-volume case.
Technical Chapter

12. Release savings only after verification

Release cost changes through evidence gatesEVT / DVT: Validate requirements: Freeze interfaces; PVT: Qualify tooling + yield: Correlate EOL screen; SOP: Control configuration: Audit drift + escapes. Process maturity and batch quantity are independent; each gate needs project-specific evidence.EVT / DVTValidate requirementsFreeze interfacesPVTQualify tooling + yieldCorrelate EOL screenSOPControl configurationAudit drift + escapes
Release cost changes through evidence gates. Process maturity and batch quantity are independent; each gate needs project-specific evidence. Scroll horizontally on small screens.

Core Engineering Conclusion

Treat a cost-down design as a new configuration with controlled qualification, not a guaranteed equivalent substitute.

Evidence, Method & Assumptions

Recommended decision method: map each changed part/process to a failure mode, acceptance test and accountable owner. The risk controls below are engineering recommendations, not a completed project risk assessment.

Release savings only after verification — decision comparison (reviewed 2026-11-02)
RiskConsequenceMitigation and alternative
Misuse: omitted output feedbackUnobserved output error or faultKeep dual feedback pending error-budget and safety validation
Cost: underfilled tooling planHigher batch cost despite cheaper BOMStage NRE; retain CNC or shared qualified tooling
Scenario mismatch: gearbox substitutionTorque/thermal or life shortfallRe-size and qualify; retain current qualified transmission
Process change: cast bearing interfacesFit/preload drift and wearRetain steel rings and validate fits under load/temperature
Engineering Boundary & Caveat:The tool cannot establish safety, supplier capability or life. A favorable fictional financial result is not release authorization.
Recommended Sourcing Action:Keep a qualified fallback design until the proposed configuration passes its agreed technical and financial gates.
Technical Chapter

13. Compare ball and roller screws with part-specific data

Select a screw using the actual dutyAxial requirements: Force + speed + stroke: Impact + supports; Part-specific sizing: Diameter + lead + life: Lubrication + preload; Acceptance tests: Accuracy + stiffness: Shock + fatigue. No universal shock multiplier or price is claimed. Ball-screw acceptance standards do not certify a roller-screw design.Axial requirementsForce + speed + strokeImpact + supportsPart-specific sizingDiameter + lead + lifeLubrication + preloadAcceptance testsAccuracy + stiffnessShock + fatigue
Select a screw using the actual duty. No universal shock multiplier or price is claimed. Ball-screw acceptance standards do not certify a roller-screw design. Scroll horizontally on small screens.

Core Engineering Conclusion

Choose screw diameter, lead, supports and load capacity from the actual axial duty and shock envelope.

Evidence, Method & Assumptions

Tolomatic’s selection guide ties screw sizing to axial force and distinguishes accuracy, repeatability and backlash. ISO 3408-3 covers ball-screw acceptance tests. Neither source establishes a universal 3.2× load advantage, 500% shock survival or a price floor.

Compare ball and roller screws with part-specific data — decision comparison (reviewed 2026-11-02)
OptionCompare on equal conditionsUnknown here
Ball screwAxial load spectrum, speed, accuracy and support layoutQualified life and delivered price
Planetary / inverted roller screwSame envelope plus nut/roller constructionImpact tolerance and production yield
Acceptance planLead error, backlash, stiffness and fatigueNo universal axial-play limit asserted
Engineering Boundary & Caveat:A generic screw label does not establish humanoid landing survival. Static impact, lubrication, buckling, supports and life require part-specific analysis.
Recommended Sourcing Action:Request a full assembly quote with lead accuracy, preload, support bearings, lubrication plan and documented shock/life acceptance.
Technical Chapter

14. Distinguish DC bus current from phase current

Ideal DC input at fixed 1.2 kW48 V DC bus: 25 A input: Cable loss ratio 1.00; 72 V DC bus: 16.67 A input: Cable loss ratio 0.444; 96 V DC bus: 12.5 A input: Cable loss ratio 0.25. DC input only: P/V. Same cable resistance gives I²R ratios 1, 0.444, 0.25. Motor phase current is a separate calculation; no efficiency, mass or safety level is inferred.48 V DC bus25 A inputCable loss ratio 1.0072 V DC bus16.67 A inputCable loss ratio 0.44496 V DC bus12.5 A inputCable loss ratio 0.25
Ideal DC input at fixed 1.2 kW. DC input only: P/V. Same cable resistance gives I²R ratios 1, 0.444, 0.25. Motor phase current is a separate calculation; no efficiency, mass or safety level is inferred. Scroll horizontally on small screens.

Core Engineering Conclusion

Higher bus voltage reduces DC input current at fixed input power. It does not automatically reduce motor torque-producing phase current.

Evidence, Method & Assumptions

Illustrative ideal DC arithmetic: 1,200 W / 48 V = 25 A; /72 V ≈ 16.67 A; /96 V = 12.5 A. With the SAME DC cable resistance, 96 V gives one quarter of 48 V cable I²R loss. TI’s motor-control guide explains torque-producing q-axis current.

Distinguish DC bus current from phase current — decision comparison (reviewed 2026-11-02)
DC voltageIdeal DC input at 1.2 kWCable I²R ratio at SAME resistance
48 V25 A1.00 (baseline)
72 V16.67 A0.444
96 V12.5 A0.25
Engineering Boundary & Caveat:This excludes conversion losses and transients. Reducing wire area increases resistance; phase current depends on motor/control/duty. No harness mass saving, inverter efficiency or PL is inferred.
Recommended Sourcing Action:Check bus input and phase currents separately; validate insulation, voltage margin, connectors, regeneration, EMI and safety functions before raising voltage.
Illustrative Scenarios

Reproducible Cost Discussion Scenarios

Fictional examples calculated from the same tool presets. No measured customer results or supplier prices are claimed.

Illustrative scenario: Biped Knee High-Torque Joint (PVT)

Engineering Premise:150 units for bipedal walking validation. High torque strain wave gear, progressive die stator, and calibrated magnetic encoders. All costs below are fictional; equivalent performance is unverified.
Technical Implementation:Select this preset in the tool. Batch 150; baseline recurring $3546; proposed recurring $1353; package NRE $94500.
Outcome & ROI:Effective unit cost including NRE: $1983. Net batch savings: $234450; negative means higher cost. Package payback: 44 units at fixed process assumptions. Obtain quotes and qualify the design before release.

Illustrative scenario: Dexterous Arm Elbow Joint (DVT)

Engineering Premise:50 units for lightweight manipulation arm. Compact harmonic drive, integrated GaN driver, and off-axis inductive encoders. All costs below are fictional; equivalent performance is unverified.
Technical Implementation:Select this preset in the tool. Batch 50; baseline recurring $2700; proposed recurring $1621; package NRE $41000.
Outcome & ROI:Effective unit cost including NRE: $2441. Net batch savings: $12950; negative means higher cost. Package payback: 38 units at fixed process assumptions. Obtain quotes and qualify the design before release.

Illustrative scenario: Ankle Linear Actuator Pushrod (PVT)

Engineering Premise:200 units for high-dynamic ankle pitch/roll differential. Inverted roller screw with co-axial frameless motor. All costs below are fictional; equivalent performance is unverified.
Technical Implementation:Select this preset in the tool. Batch 200; baseline recurring $3828; proposed recurring $1559; package NRE $100500.
Outcome & ROI:Effective unit cost including NRE: $2061.5. Net batch savings: $353300; negative means higher cost. Package payback: 45 units at fixed process assumptions. Obtain quotes and qualify the design before release.

Illustrative scenario: Mass-Scale QDD Joint Module (SOP)
Engineering Premise:5,000 units for agile dynamic humanoid robot. Planetary QDD with MIM gears, hairpin stator, and consolidated housing. All costs below are fictional; equivalent performance is unverified.
Technical Implementation:Select this preset in the tool. Batch 5000; baseline recurring $3546; proposed recurring $726; package NRE $190000.
Outcome & ROI:Effective unit cost including NRE: $764. Net batch savings: $13910000; negative means higher cost. Package payback: 68 units at fixed process assumptions. Obtain quotes and qualify the design before release.
Actuator cost model software run showing unit cost including NRE and net batch savings at 150 units
Original software run, November 2, 2026: Biped Knee PVT preset, 150 units, all seven preset architecture assumptions unchanged, supplier price and NRE left unknown. Reproduce with Reset Defaults. Only the result panel is captured; site navigation is outside the crop. Fictional USD arithmetic, not measured actuator performance, a supplier quote, or a customer outcome.
Decision Guidance

Frequently Asked Engineering & Sourcing Questions

Technical answers to common cost modeling, tooling NRE, and procurement questions.

Cost Modeling

Is this a price forecast?

No. The baseline, multipliers and NRE are fictional teaching inputs. They demonstrate cost mechanisms, not supplier prices. Use the separate quote fields for your own dated offer.

Cost Modeling

Does a lower BOM always save money?

No. Include one-time tooling, qualification, expected scrap and delivered charges. The tool shows effective unit cost and net batch savings; a negative value means the example proposal costs more.

Cost Modeling

Does changing batch quantity create a discount?

No. Quantity only changes fixed-cost allocation and totals. Process-stage coefficients stay fixed until you change the assumed maturity stage.

Cost Modeling

What does package payback mean?

The smallest whole quantity covering the example package NRE from positive recurring savings. It assumes the baseline has no incremental NRE and excludes financing and unquoted costs.

Cost Modeling

How do I enter a supplier quote?

Enter both the recurring unit price and one-time NRE in USD, up to two decimal places. Enter zero NRE only if confirmed. The subtotal is quantity × price + NRE; it is separate from fictional model costs.

Technical Tradeoffs

Can I remove the output encoder?

Only after the installed error budget and required fault response are validated. Input sensing alone does not directly measure output lost motion or deflection.

Technical Tradeoffs

Can rollers run directly on a cast shell?

Do not assume an aluminium or magnesium casting is a qualified raceway. Retain hardened steel rings unless a bearing specialist validates material, surface, preload and life.

Technical Tradeoffs

Does 96 V halve motor phase current?

Not by itself. At fixed input power it halves ideal DC bus current relative to 48 V. Phase current is set by motor torque, winding design and control conditions.

Technical Tradeoffs

Does GaN establish PL d?

No. A semiconductor choice does not determine a system safety Performance Level. Define required safety functions, architecture, diagnostics and validation for the complete design.

Technical Tradeoffs

Can the calculator compare equal-performance gearboxes?

It compares fictional cost assumptions only. Re-size the motor and qualify output load, speed, thermal behavior, accuracy and life before changing transmission.

Technical Tradeoffs

Will potting justify a smaller motor?

That is unknown until matched thermal tests establish a safe operating margin. Include cure, inspection, scrap and repair costs in the comparison.

Tooling & NRE

Is package payback a stator-die threshold?

No. Compute stator-specific payback using incremental die NRE and verified per-stack savings. The package result includes transmission, feedback, housing, electronics and assembly tooling.

Tooling & NRE

What if committed volume falls?

Recalculate at the lower quantity. Consider CNC, soft tooling or an existing platform until demand and the design are stable enough to fund hard tooling.

Tooling & NRE

Who owns the tooling?

Agree ownership, maintenance, storage, design-change charges and transfer rights in writing. These terms are not determined by the tool.

Sourcing & RFQ

What should an RFQ include?

Send drawing revision, STEP/GD&T, torque-speed duty, cooling, output accuracy, life/load spectrum, fault response, quantities, destination and required acceptance records.

Sourcing & RFQ

Can a short EOL screen prove continuous torque?

No. Correlate a short production screen with separate thermal equilibrium and life qualification. Keep audit testing and serialized results.

Sourcing & RFQ

Are the scenarios customer success stories?

No. They use the same fictional calculator presets and are reproducible arithmetic examples. No measured customer savings are claimed.

Sourcing & RFQ

Do the standards prove the modeled savings?

No. The linked publisher/manufacturer references support technical scope and boundaries. They do not supply the model’s costs or certify an actuator design.

Literature & Standards

Primary Engineering Standards & Industry References

Publisher and manufacturer references checked November 2, 2026. These support technical boundaries, not modeled prices. Public summaries do not replace the complete standards or design validation.

IEC 60034-1:2026 — Rotating electrical machines: Rating and performance

Motor rating and performance reference. Edition 15 replaces the 2022 edition.

Boundary: The public catalogue establishes edition and scope, not actuator prices or a project-specific thermal rating.

ISO 13849-1:2023 — Safety-related control systems: Design principles

Methodology for designing and integrating safety-related control systems, including software.

Boundary: Neither a GaN transistor nor an encoder count establishes a Performance Level. Determine required safety functions and validate the complete design.

ISO 3408-3:2006 — Ball screws: Acceptance conditions and tests

Acceptance conditions and permissible deviations for ball-screw tests.

Boundary: This is a ball-screw standard, not proof of roller-screw shock capability or a universal axial-play limit.

Schaeffler Technical Pocket Guide — Raceway material selection

The material-selection section explains the hardness, hardened depth and cleanliness requirements of rolling raceways.

Boundary: Apply the selected bearing manufacturer’s design requirements. A cast aluminium bearing seat is not a qualified rolling raceway.

Texas Instruments TIDM-02018 — Motor control design guide

System Design Theory distinguishes torque-producing q-axis current and motor voltage constraints.

Boundary: Motor phase current cannot be inferred from DC bus voltage alone. The power example below describes DC input current only.

Tolomatic — Selecting the Optimal Screw Technology

Manufacturer selection guide covering axial force, screw diameter, lead accuracy, repeatability and backlash.

Boundary: Family-level capabilities do not qualify any humanoid joint. Obtain a part-specific load/life calculation and impact test; pricing remains unknown.

Request an Actuator Cost Reduction DFM Review

Send your 3D STEP assembly, 2D GD&T drawings, and annual volume target. Ask for a feasibility review, itemized recurring costs, tooling NRE, and acceptance scope. Price, capability and delivery require project-specific confirmation.

Inquiry Email

[email protected]

Include target torque/speed, quantity, and delivery location.

Application Engineer

WhatsApp Engineering Support

Talk directly about drawings, torque-speed targets, and RFQ data gaps.